Engineered for high-density storage environments across Encamp's industrial and distribution zones.
Analyzing structural demand, operational bottlenecks, and vertical density requirements in the regional supply chain.
The Encamp market has evolved into a vital trade node, driven by rapid industrialization, regional manufacturing clusters, and third-party logistics (3PL) expansion. As land utilization costs increase across key commercial sectors in Encamp, enterprise warehouse managers are aggressively shifting from traditional floor stacking to vertical structural racking architectures to optimize volumetric storage efficiency.
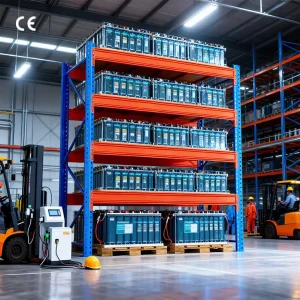
Distribution centers within Encamp require heavy-duty storage infrastructure capable of handling high throughput frequencies, mixed-pallet stock keeping units (SKUs), and extreme weight profiles. Equipment deployed in local facilities must withstand ambient humidity variations, heavy forklift impact risks, and continuous cycle fatigue without structural compromise.
Procurement teams in Encamp prioritize structural integrity verified through Finite Element Analysis (FEA) and stringent deflection standard limits ($L/200$). Factory-certified racking systems certified against ISO 9001 and international safety standards ensure operational risk mitigation against structural failure under maximum load capacity limits.
How technical specifications directly govern load stability, seismic safety, and longevity under heavy usage.
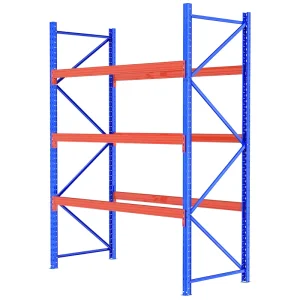
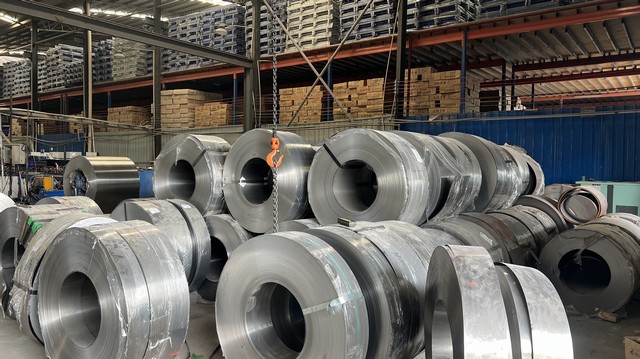
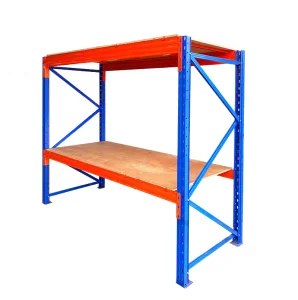
The foundation of reliable heavy-duty shelving lies in the raw material composition. Industrial pallet racking systems manufactured for the Encamp market utilize high-grade cold-rolled structural steel (Q235B and Q355B). Cold rolling increases yield strength and structural rigidity, ensuring upright frames maintain dimensional tolerance even under concentrated loads scaling up to 5,000 kg per beam level.
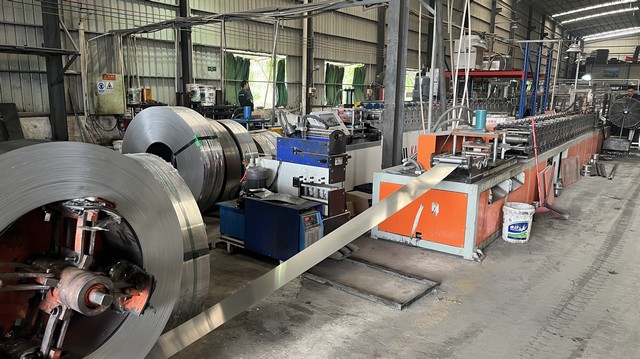
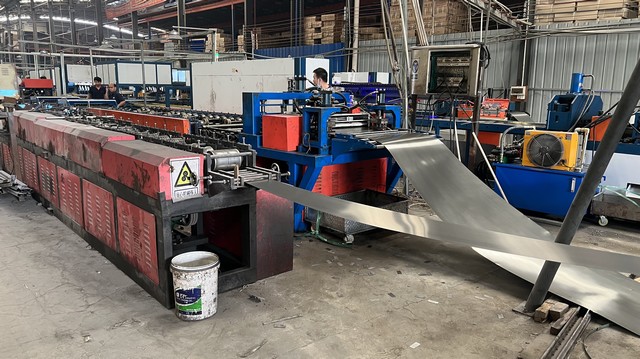
Integrating raw material processing, automated rolling production, quality assurance, and global export logistics.
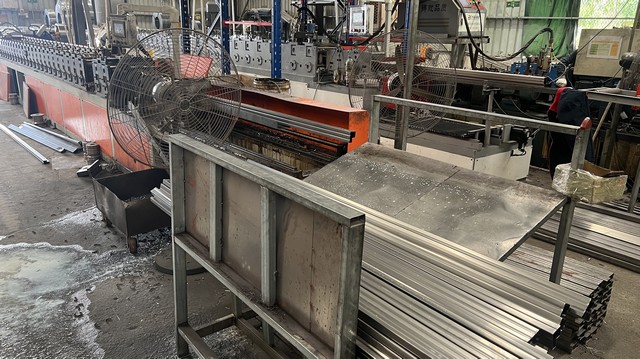
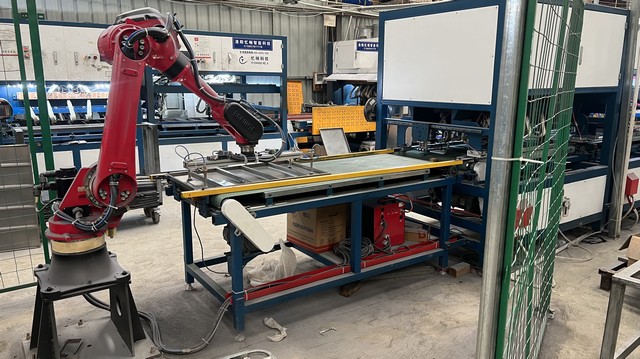
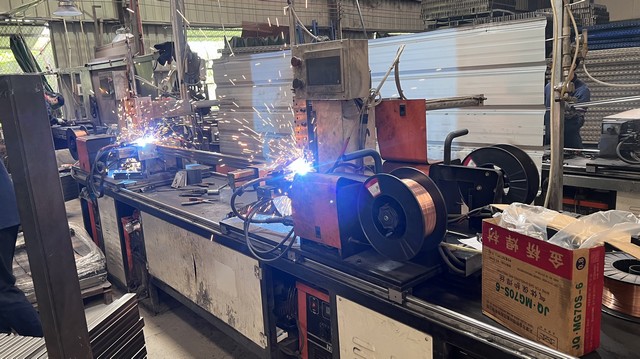
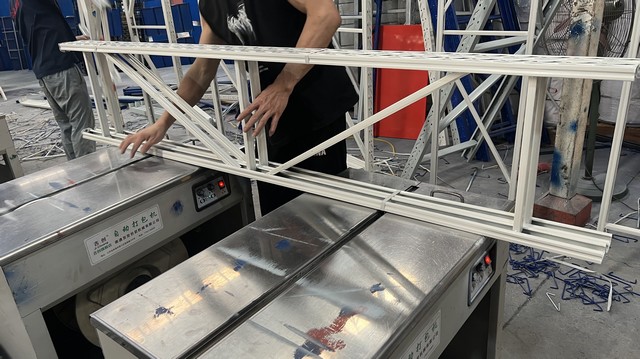
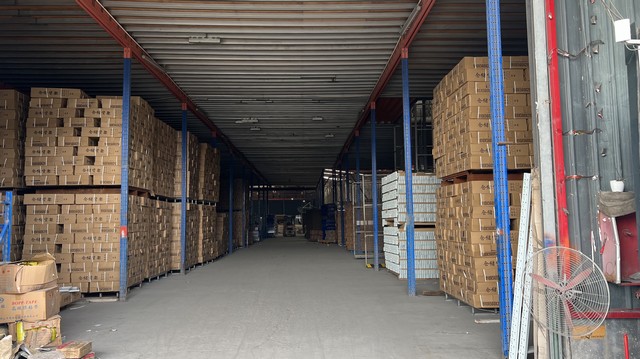
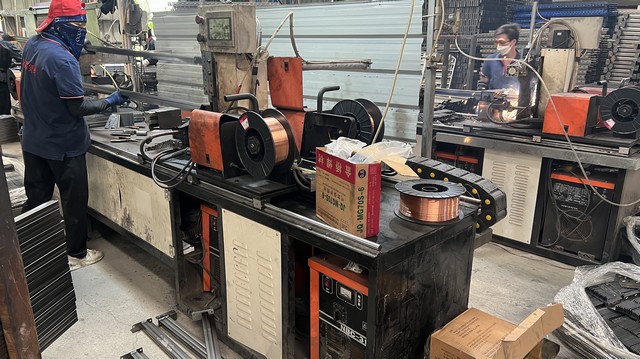
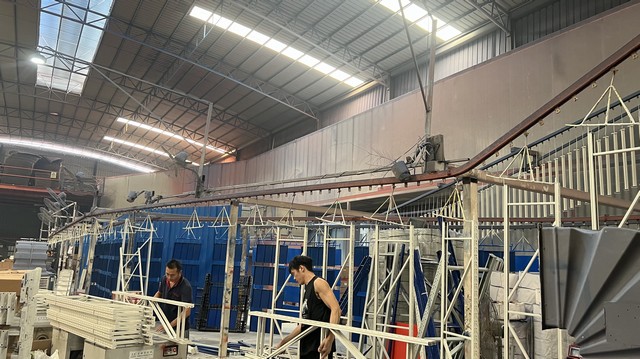
Established in 2013, Guangzhou Fangjiu Shelf Co., Ltd. is a leading manufacturer specializing in heavy-duty warehouse racking systems, industrial shelving, and customized storage solutions. Spanning a modern facility of over 35,000 square meters, we integrate raw material processing, automated production, strict quality inspection, and global distribution under one roof.
With 10 years of deep industry expertise and 7 years of export experience, our brand has grown into a trusted storage solution supplier worldwide. Our products are exported to primary markets across North America, Europe, Southeast Asia, and the Middle East, generating an annual export revenue reaching $49 million USD. We maintain robust strategic alliances with over 580 reliable supply chain partners to ensure seamless sourcing, consistent material quality, and competitive lead times.
Quality and safety are at the core of our operations. Our dedicated quality assurance division comprises 38 professional QC inspectors who enforce stringent quality control protocols at every manufacturing stage. Utilizing advanced testing methods—including Ultrasonic Flaw Detection for critical welds, Salt Spray Corrosion Testing, Automated Powder Coating Coating Thickness Measurement, and Full Load Stress & Deflection Testing—we ensure every rack system meets ISO 9001 and international safety standards.
We cater to a diverse clientele, primarily serving B2B enterprise buyers, third-party logistics (3PL) providers, industrial warehouse developers, and global racking importers. Backed by a professional team of 25 R&D engineers, we possess robust research and development capabilities, successfully launching over 150 new innovative products and structural designs in the past year alone. Our comprehensive OEM & ODM customization options allow clients to tailor beam capacities, upright profiles, decking types, color schemes, and specialized anti-seismic rack structures to meet precise warehouse layout requirements. At Guangzhou Fangjiu Shelf Co., Ltd., we deliver reliable, space-efficient, and durable storage rack solutions tailored to scale your operational efficiency.
Custom structural configurations engineered for specific vertical industries in Encamp.
Utilizing Drive-In and Very Narrow Aisle (VNA) heavy-duty systems to maximize cold storage volume ratio by up to 80%. Anti-frost powder coatings prevent micro-cracking in sub-zero temperature environments common to cold chain hubs in Encamp.
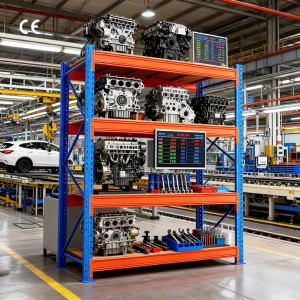
Cantilever and heavy box-beam rack configurations accommodate non-standard length payloads, engine blocks, steel coils, and spare parts with up to 5,000kg single-tier load ratings, engineered to withstand violent forklift handling cycles.
Multi-level heavy-duty mezzanine rack structures integrate footbridges, handrails, and automated conveyers. These systems convert high-ceiling Encamp warehouses into multi-story picking centers with maximum vertical utilization.
How heavy-duty shelving is evolving to support Next-Gen AS/RS and AI-driven inventory logistics in Encamp.
Automated Storage and Retrieval Systems (AS/RS) require millimetric precision tolerances in rack fabrication. Upright profile deflection and beam level accuracy must meet zero-margin tolerances for stacker crane navigation.
Modern racking structures installed in primary Encamp fulfillment hubs are increasingly fitted with strain gauges and vibration sensors to detect dynamic structural fatigue and prevent load collapse risks in real time.
Transitioning from traditional solvent painting to thermosetting epoxy powder coating lines ensures zero VOC emissions during manufacturing, aligning with Encamp enterprise ESG compliance mandates.
Key technical considerations when issuing Request for Proposals (RFQs) for Encamp warehouse infrastructure.
Verify structural load calculations per pallet position. Select column widths (80mm to 120mm) and beam profile heights (80mm to 160mm) corresponding to point load stress requirements.
Ensure warehouse concrete slab rating matches localized point loading exerted by baseplates. Utilize high-tensile anchor bolts for seismic anchoring.
Specify galvanized finish for outdoor/humid applications or high-durability epoxy electrostatic powder coat for standard ambient distribution facilities.
Ensure knockdown structure design allows maximum packing density in standard 40ft High Cube containers, minimizing ocean freight costs per unit.
Expert answers addressing structural specifications, custom manufacturing, logistics, and installation safety.
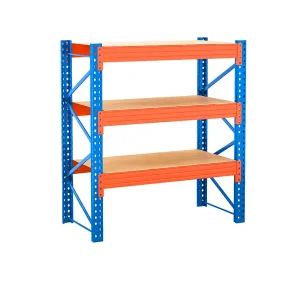
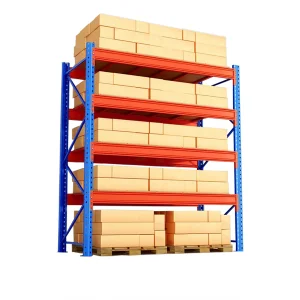
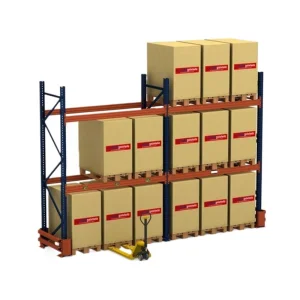
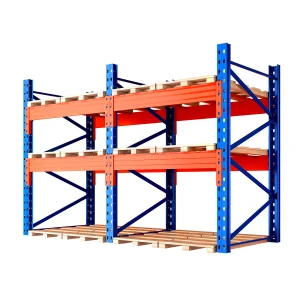
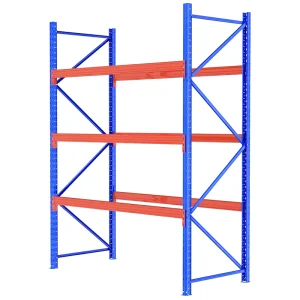
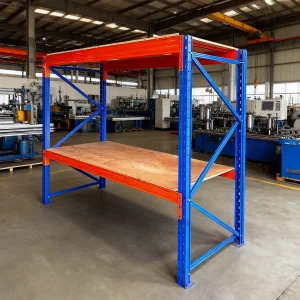
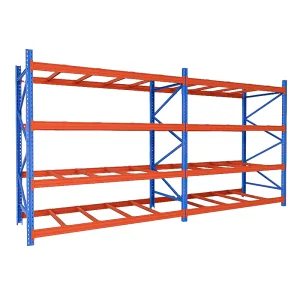
Explore our complete inventory of industrial-grade heavy-duty storage shelving units for Encamp enterprises.
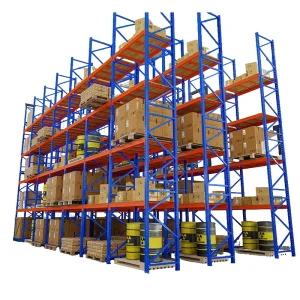
Contact Guangzhou Fangjiu Shelf Co., Ltd. today for custom rack CAD engineering layout drawings, factory-direct OEM pricing, and comprehensive technical RFQ support.
Send Inquiry Now Fangjiu Rack